Step-by-Step Guide: Fabricating with ASTM F136 Grade 23 Titanium Bars
Introduction to ASTM F136 Grade 23 Titanium Bars
For medical‑device OEM factories, implant manufacturers and global procurement managers, mastering fabrication workflows for ASTM F136 Grade 23 Titanium Bar directly determines finished‑implant yield, safety and compliance. ASTM F136 Grade 23 (Ti‑6Al‑4V ELI, UNS R56401) is forged medical‑grade Titanium Alloy for permanent surgical implants. Compared with standard Grade5 Titanium Rod, it enforces strict limits on interstitial elements such as oxygen, hydrogen, nitrogen and carbon. PSX Baoji Pengshengxin Non‑Ferrous Metal Co., Ltd supplies this critical implant‑grade bar alongside our full‑range Titanium Material, Titanium Forging, Titanium CNC Machining, Titanium Tube and Titanium Flange product portfolio for worldwide medical‑device supply chains.
Understanding Material Properties and Applications
Core Physical‑Mechanical Advantages of Grade 23
- Ultra‑low oxygen content ≤0.13% (ELI specification), higher fracture toughness and reduced cold‑brittleness risk versus Grade5
- Excellent biocompatibility: non‑allergenic, non‑cytotoxic, minimal ion leaching for long‑term in‑vivo implantation
- High specific strength, low elastic modulus close to human bone to mitigate stress‑shielding effects
- Superior fatigue‑crack‑propagation resistance for cyclic‑load orthopedic and spinal implant components
- Homogeneous forged microstructure, segregation‑free, well‑suited for turning, milling, deep‑hole drilling and precision Titanium CNC Machining
- Full‑batch non‑destructive testing (UT ultrasonic + MT magnetic‑particle) to eliminate internal shrinkage cavities, inclusions and surface cracks
Key End‑Use Application Scenarios
- Orthopedic trauma implants: LCP bone screws, reconstruction‑plate blanks, intramedullary‑nail system raw stock, surgical suture anchors
- Spinal‑surgery components: pedicle‑screw connecting rods, scoliosis correction rods, intervertebral‑fusion‑device fasteners
- Joint‑reconstruction implants: hip / knee / shoulder prosthesis fixing fasteners and partial forging blanks
- Dental implant manufacturing: φ3‑φ6 mm centerless‑ground polished bar for implant fixtures, abutments and micro retention screws
- Cranio‑maxillofacial surgical fixation hardware, sports‑medicine minimally‑invasive implant components
- Custom‑patient‑matched implant blanks, university R&D test specimens, instrument blanks for high‑vibration surgical tools
Safety Precautions and Equipment Needed
Fabricating ASTM F136 Grade 23 Titanium Bar creates fine titanium dust, high cutting heat and chip‑fire risks; medical‑grade production requires strict operator and workstation safety protocols.
Mandatory Safety Precautions
- Wear approved respiratory dust‑mask, safety goggles, cut‑resistant gloves and flame‑resistant work clothing; avoid skin contact with sharp hot titanium chips
- Install local dust‑extraction ventilation for titanium fine‑dust collection; never allow accumulated dry titanium swarf to build‑up inside machines
- Prepare class‑D metal‑fire extinguishing media; water‑based extinguishers are ineffective against titanium‑chip ignition hazards
- Isolate medical‑grade bar‑stock processing zones from general‑industrial titanium production to prevent cross‑grade material contamination
Recommended Equipment & Tooling List
- CNC lathes / vertical machining centers for turning, milling and deep‑hole‑drilling operations
- Carbide tool inserts optimized for titanium‑alloy cutting; avoid standard general‑purpose steel‑cutting tooling
- High‑pressure, stable‑flow titanium‑specialized cutting‑coolant delivery system
- Precision band‑saw for bar blanking; centerless‑grinding machines for surface finishing
- Metrology equipment: micrometers, optical comparators, hardness testers; UT / MT non‑destructive‑testing apparatus for QC validation
Preparing Your Workspace for Fabrication
Workspace preparation directly impacts medical‑device audit traceability and finished‑part quality when working with ASTM F136 Grade23 bar‑stock.
- Incoming material verification: Match received bar batches against supplier MTR, spectroscopic‑analysis report and UT‑MT inspection documents; cross‑check heat‑lot numbers for full traceability (ISO13485 requirement).
- Workstation segregation: Use dedicated fixtures, vices and coolant circuits for medical‑grade titanium; do not share tooling previously used for carbon‑steel or non‑medical‑grade titanium‑alloy to eliminate iron‑contamination risk.
- Surface protection: Keep original protective packaging until right‑before machining; handle polished bar surfaces with non‑marring soft jaws to prevent scratches which become fatigue‑failure initiation points for implant parts.
- Batch‑record system: Establish digital or physical production logs linking each bar lot number to blanking, machining, finishing and inspection records for regulatory audits.
Cutting Techniques for Titanium Bars
Improper cutting of ASTM F136 Grade 23 Titanium Bar may induce surface micro‑cracks and residual stress that cannot be tolerated for permanent implant raw‑stock.
Band‑Saw Blanking Best‑Practice Steps
- Select bi‑metal or carbide‑tipped band‑saw blades designed for titanium‑alloy cutting; set lower linear blade speed versus steel cutting parameters.
- Apply continuous abundant coolant across the full cutting zone to dissipate high frictional heat.
- Secure bar stock rigidly to eliminate workpiece vibration and chatter during sawing.
- After cutting blanks, remove saw‑edge burrs carefully; inspect cut ends visually for micro‑tears, cracking or thermal discoloration.
- Tag each blank segment with parent‑batch heat‑lot ID to maintain full‑process traceability.
Note: Avoid abrasive‑wheel cutting for medical‑grade Grade23 bar; abrasive‑cutting can embed abrasive‑particle contamination and introduce harmful residual surface stress.
Drilling and Machining Best Practices
Ti‑6Al‑4V ELI generates high cutting heat and is prone to built‑up‑edge (BUE) on cutting tools; stable parameter settings are essential for mass‑production of implant‑grade components from Titanium Bar.
Turning & Milling Guidelines
- Use sharp carbide tools for titanium‑alloy; maintain moderate cutting speed, moderate feed‑rate and deep‑enough depth‑of‑cut to prevent tool rubbing the workpiece surface.
- Deliver high‑volume cutting coolant directly onto tool‑chip interface zone to take away heat rapidly.
- Minimize tool overhang to suppress machining chatter which creates wavy surface texture harmful for cyclic‑load implant parts.
Deep‑Hole Drilling Recommendations
- Adopt titanium‑optimized drill geometry; use peck‑drilling cycles for deep holes to facilitate chip evacuation and prevent drill‑bit overheating.
- Monitor drill‑bit wear continuously; replace tools at defined wear thresholds rather than running until catastrophic failure.
- After drilling, deburr hole‑entry and hole‑exit edges completely; inspect for micro‑cracks at hole‑corners.
Welding Procedures for Grade 23 Titanium
For medical permanent‑implant‑grade applications, as‑received ASTM F136 Grade 23 Titanium Bar is almost exclusively used as solid‑bar for subtractive‑machining; welding is rarely performed on final implant blanks. If welding operations are required for secondary non‑implant components:
- Use full‑penetration gas‑shielded GTAW (TIG) welding with high‑purity argon shielding; strictly exclude oxygen / nitrogen contamination during molten‑metal cooling phase.
- Thoroughly clean bar‑joint surfaces by solvent degreasing; eliminate oil, fingerprints and surface oxides before welding starts.
- Post‑weld non‑destructive inspection (UT, MT) is mandatory; reject weld zones showing oxidation discoloration, porosity or cracking.
- Important reminder: Welded sections of Grade23 material generally cannot be used for permanent human‑body load‑bearing implant parts due to potential toughness degradation in weld‑heat‑affected zones.
Surface Finishing and Polishing Methods
Surface finish directly influences implant‑component biocompatibility, fatigue‑life and anti‑ion‑leaching performance. PSX supplies ASTM F136 Grade 23 Titanium Bar with multiple as‑supplied surface options: hot‑rolled, precision‑turned, ground and centerless‑bright‑polished.
- Centerless‑grinding: Primary process for small‑diameter dental‑implant bar stock (φ3‑φ6 mm); delivers consistent dimensional accuracy and uniform bright metallic surface, removing surface‑layer defects.
- Precision turning: For medium‑large‑diameter bar blanks for orthopedic‑implant pre‑forms.
- Mechanical polishing: Progressive grit sequence; final polishing must eliminate all tool‑lines and micro‑scratches for implant‑part pre‑cursors.
- Post‑finishing cleaning: Complete solvent / alkaline cleaning to fully remove polishing‑media residues before parts move to QC inspection; avoid residual abrasive particle entrapment.
Quality Control and Inspection Guidelines
Quality‑control workflows for fabricating ASTM F136 Grade23 titanium bar‑derived components must align with ASTM F136 and ISO13485 medical‑supply‑chain requirements.
- Document traceability audit: Confirm heat‑lot number linkage from original incoming bar stock through each fabrication step.
- Dimensional inspection: Verify diameter, length, chamfer and tolerance against customer drawing specifications.
- Visual surface inspection: Screen for scratches, tears, thermal discoloration, burrs and contamination residues.
- Non‑destructive‑testing: UT ultrasonic inspection for internal defects; MT magnetic‑particle inspection for surface‑breaking cracks (mandatory for implant‑grade bar‑stock and critical semi‑finished blanks).
- Random spectroscopic‑composition spot‑checks to confirm interstitial‑element levels meet Grade23 ELI oxygen ≤0.13% limits.
- Archive all inspection reports together with MTR material‑test certificates for customer and regulatory‑audit access.
Common Challenges and Troubleshooting Tips
Troubleshooting Table for ASTM F136 Grade 23 Titanium Fabrication
- Problem: Excessive built‑up‑edge (BUE) on cutting‑tools
Root cause: Incorrect cutting‑speed / insufficient coolant.
Solution: Reduce cutting‑speed; boost coolant flow rate; use fresh sharp titanium‑grade carbide inserts. - Problem: Machining chatter / wavy workpiece surface
Root cause: Long tool overhang, weak fixture clamping.
Solution: Shorten tool overhang; rigidly clamp bar‑stock; optimize spindle‑speed parameters. - Problem: Surface micro‑scratches on polished bar blanks
Root cause: Poor workpiece handling, dirty grinding media.
Solution: Use soft non‑metallic jaw fixtures; filter grinding‑fluid circulation loops; implement protective‑film handling procedures. - Problem: Chip ignition / over‑heating chips
Root cause: Inadequate coolant coverage.
Solution: Re‑align coolant nozzles directly at tool‑chip interface; enforce good swarf‑removal housekeeping rules. - Problem: Batch‑to‑batch subtle machining‑variation
Root cause: Inconsistent raw‑material microstructure or tool‑wear drift.
Solution: Source bar‑stock from certified suppliers such as PSX with full‑forging‑process‑traceability; implement scheduled‑tool‑change protocols.
Industry Latest Technical Updates
Global medical‑titanium supply‑chain and fabrication industries are accelerating digital traceability deployment for implant‑grade titanium bar‑stock. Increasing North‑American and European medical‑device auditors demand fully‑digitized MTR, NDT and spectroscopic archives rather than only paper‑based documentation. Optimized forging workflows lower segregation risk for small‑diameter medical‑grade bars used in high‑end dental OEM production. Hybrid manufacturing workflows combining wrought ASTM F136 Grade 23 bar blanks plus additive‑manufacturing post‑processing gain wider adoption for patient‑specific custom‑implant projects. Many manufacturers are upgrading inline automated surface‑defect‑inspection stations to decrease human‑inspection error risk for high‑value implant raw‑material batches.
Key Procurement Concerns for European & American Buyers
Procurement managers representing EU and US medical OEM factories focus on five core evaluation criteria while sourcing ASTM F136 Grade 23 Titanium Bar. First is complete, verifiable document packages: MTR material‑test certificates, UT‑MT non‑destructive‑testing records and spectroscopic‑analysis reports that satisfy ISO13485 audit evidence requirements. Second is strict dimensional‑tolerance stability, especially for small‑diameter centerless‑ground dental‑implant bar stock. Third is validated supplier‑factory quality‑system certifications such as ISO9001 and proven experience manufacturing implant‑grade titanium raw‑materials. Fourth is consistent batch‑to‑batch metallurgical performance to prevent unexpected production‑line rejects during high‑volume CNC‑machining cycles. Fifth is supplier’s dual‑capacity capability: supporting low‑volume R&D sample prototyping as well as predictable‑lead‑time large‑volume serial‑production orders.
New R&D & Application Trends
Recent material‑processing R&D continuously expands application boundaries for Ti‑6Al‑4V ELI Grade23 wrought bar‑stock. Medical OEM teams increasingly adopt forged Grade23 bar as subtractive‑machining blanks for personalized patient‑matched implants, balancing superior wrought‑material mechanical reliability compared to pure 3D‑printed titanium components. Universities and biomedical‑research institutes raise procurement volumes of Grade23 test‑bar specimens for biomechanics animal‑experiment and biomaterial‑validation projects. Another emerging application direction applies ASTM F136 Grade23 raw‑material for high‑cycle‑vibration minimally‑invasive‑surgical‑instrument core shafts, leveraging its outstanding anti‑fatigue performance. Supply‑chain participants also keep optimizing centerless‑grind and precision‑polish surface‑treatment workflows to further reduce surface‑defect rates for downstream implant‑component mass‑manufacturing.
Industry Standard Popularization
Critical Quality & Safety Specifications for ASTM F136 Grade 23 Titanium Bar
- ASTM F136‑23: Core US standard defining chemical composition, interstitial‑element limits, mechanical‑property requirements and testing protocols for wrought Ti‑6Al‑4V ELI implant‑grade titanium‑alloy bar.
- ISO 13485: Medical‑device‑supply‑chain quality‑management‑system requirement; raw‑material vendors must supply fully traceable document sets for audit purposes.
- NDT Mandates: Ultrasonic Testing (UT) detects internal voids / inclusions; Magnetic‑Particle Testing (MT) identifies surface‑breaking cracks for implant‑grade bar‑stock.
- Important distinction: ASTM B348 governs general‑industrial titanium‑bar and cannot substitute ASTM F136 for surgical‑implant raw‑material procurement.
Product Usage & Maintenance Knowledge
Storage, Handling & Scrap‑Material Management for ASTM F136 Grade 23 Titanium Bar
- Storage: Store implant‑grade bar‑stock inside dry indoor warehouses; avoid long‑term exposure to salt‑mist, moisture and corrosive vapors. Retain original anti‑scratch protective packaging until immediately before fabrication work‑start.
- Handling: Prevent impact‑knocks and surface scratches; scratches on polished bar‑surfaces can become stress‑concentration origins in finished implant‑parts.
- Scrap‑chip management: Collect titanium‑alloy machining swarf separately by material‑grade; do not mix Grade23 medical‑grade chips with general‑industrial‑grade titanium scrap. Professional‑recycling channels can re‑process clean Grade23 titanium‑chips under strict impurity‑control protocols.
- Document retention: Keep MTR, NDT reports linked to physical‑batch numbers throughout OEM production cycles to satisfy medical‑regulatory traceability‑audit demands.
Innovation in Manufacturing: PSX Factory & R&D Strength
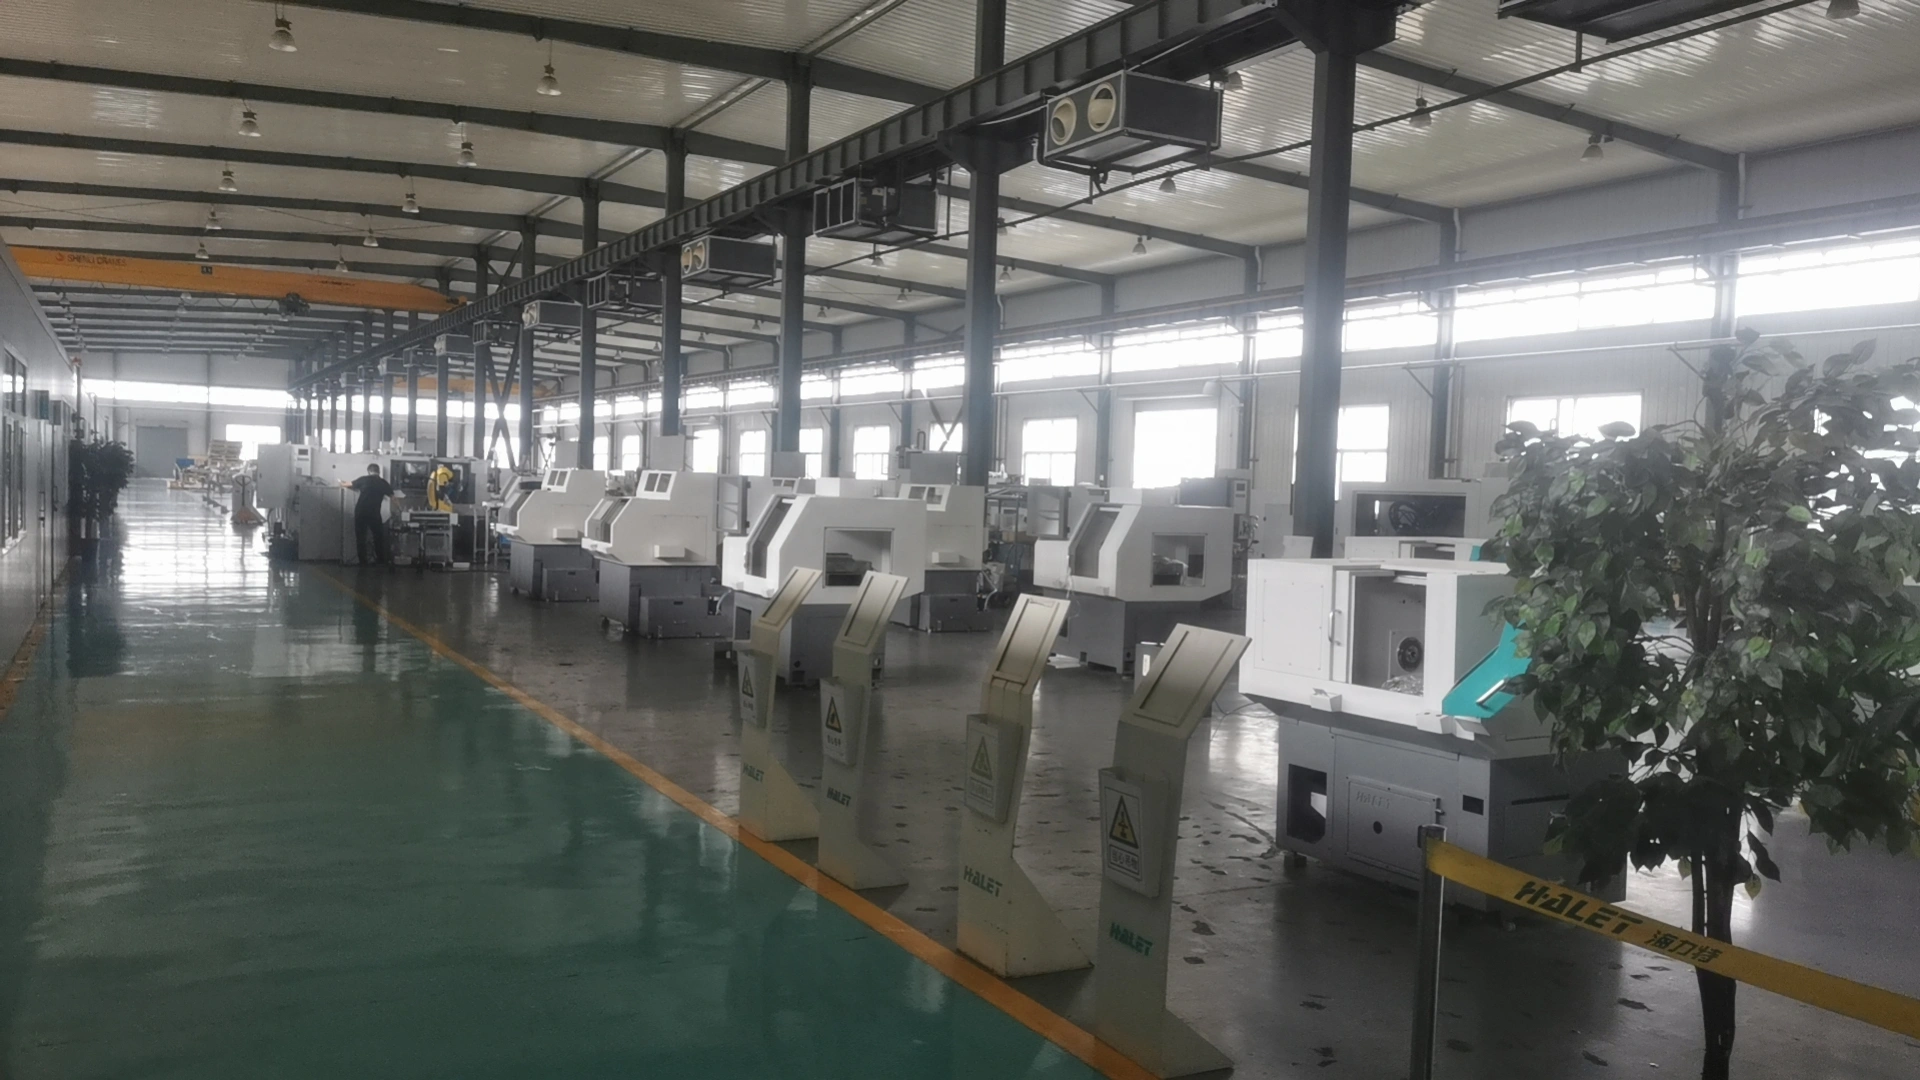
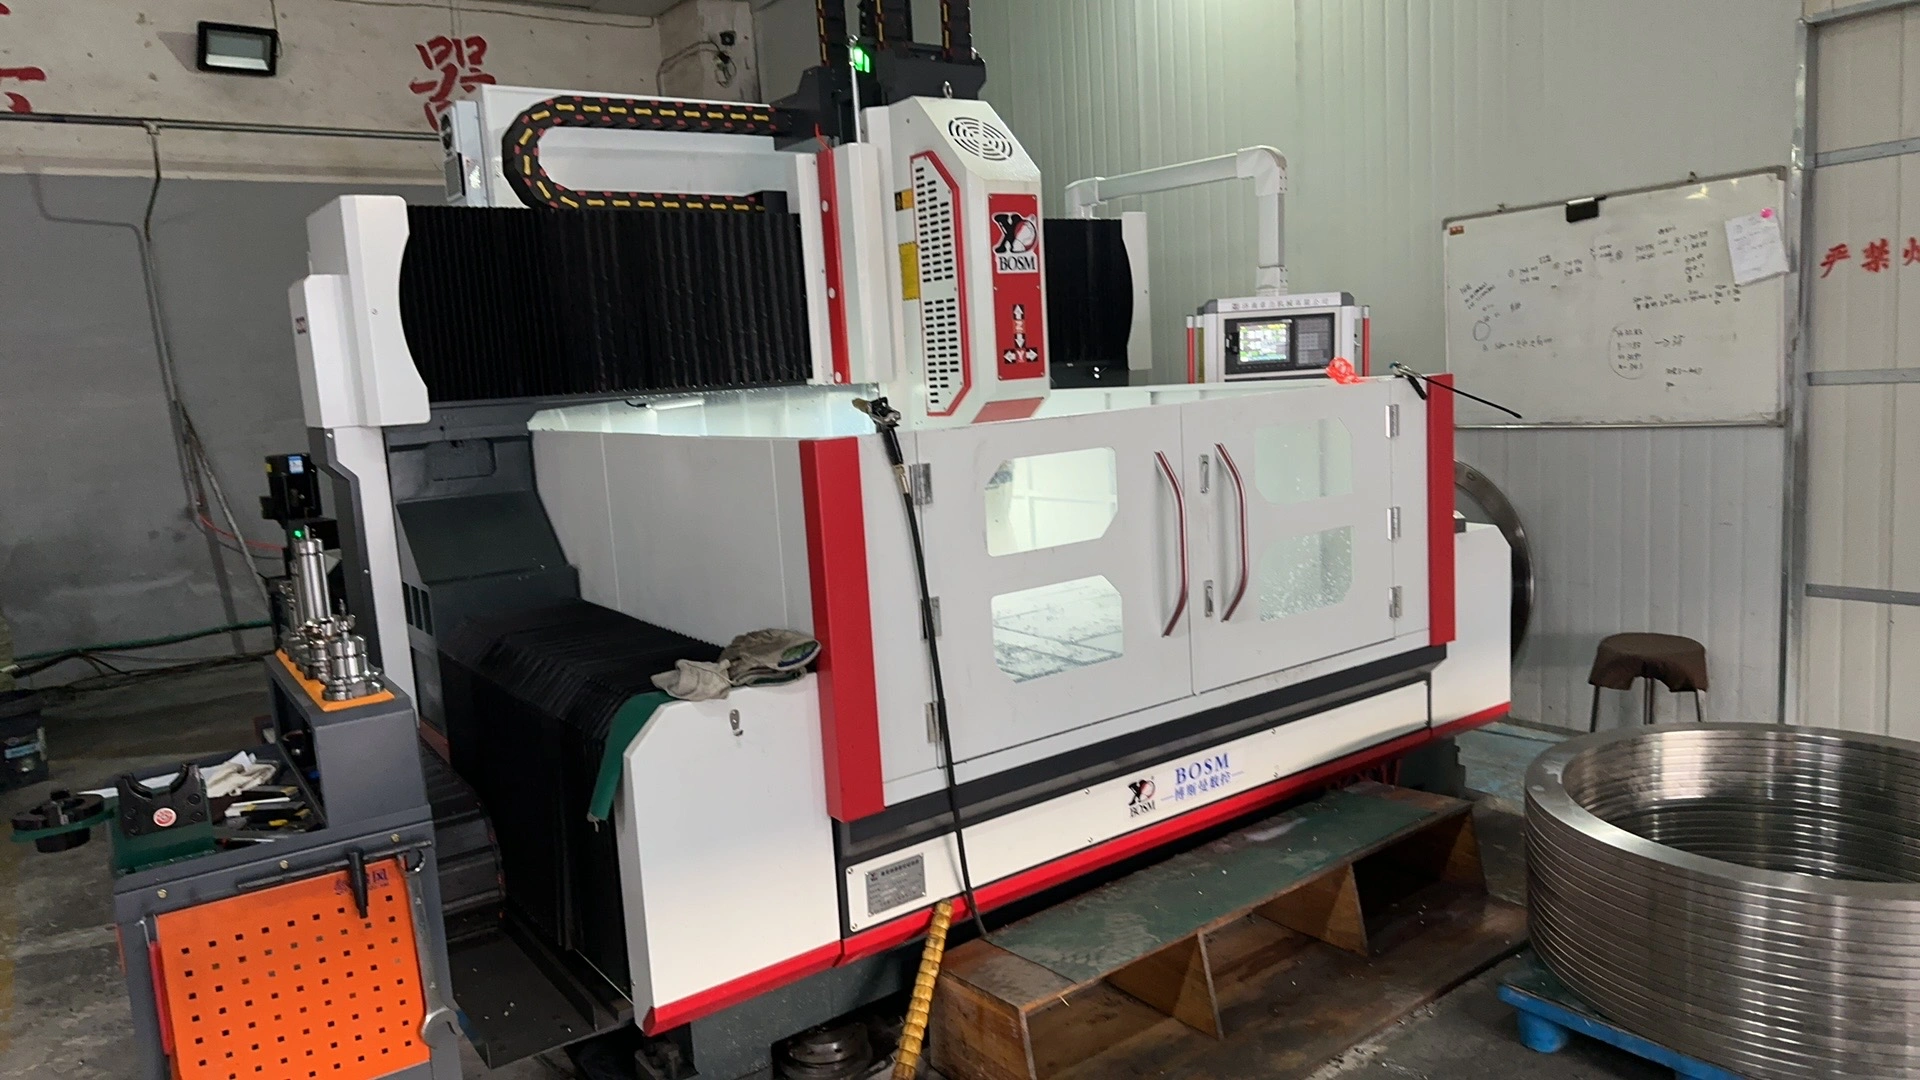
Baoji Pengshengxin Non‑Ferrous Metal Co., Ltd (PSX Brand), founded 2008, is situated in Baoji “China’s Titanium Valley”. Our factory occupies more than 5 000 m², equipped with modern workshops, imported CNC machining centers, vertical milling machines and dedicated non‑destructive‑inspection devices. Our in‑house R&D team includes over 10 professional material‑science engineers and senior experienced technicians; multiple team members hold PhD‑level technical backgrounds. We maintain ISO 9001 and GJB9001C‑2017 quality‑system certifications. Our production capacity supports both small‑batch medical‑R&D prototype orders and large‑volume serial‑production for Titanium Bar, Titanium Forging, Titanium CNC Machining and other Titanium Alloy‑based products. We offer diversified custom services: multiple surface finishes, custom cutting‑length, chamfering, peeling and centerless‑grinding for implant‑grade ASTM F136 Grade23 titanium bar‑stock.
FAQ — Frequently Asked Questions for B‑End Procurement & Fabrication Engineers
Q1: Can standard Grade5 Ti‑6Al‑4V bar replace ASTM F136 Grade 23 titanium bar for permanent implant fabrication?
A1: No. Grade23 ELI enforces far‑stricter interstitial‑element caps (oxygen ≤0.13 %), delivering higher fracture‑toughness and lower cold‑brittleness risk. Standard Grade5 shall not be substituted for permanent load‑bearing implant raw‑material.
Q2: What documentation will PSX supply with each ASTM F136 Grade 23 Titanium Bar shipment?
A2: Every batch includes original manufacturer MTR material‑test‑certificate, UT‑MT non‑destructive‑testing report and spectroscopic‑analysis report to meet ISO13485 medical‑supply‑chain traceability‑audit‑needs.
Q3: What custom specifications are supported for Grade23 titanium bar‑stock?
A3: Multiple surface finishes, custom lengths, chamfering, peeling and centerless‑grinding. We accept small‑batch R&D sample orders as well as large‑volume OEM mass‑production orders.
Q4: Can I weld ASTM F136 Grade 23 bar‑stock for finished permanent‑implant components?
A4: Weld‑heat‑affected zones degrade ELI‑grade toughness; welded sections are not acceptable for permanent load‑bearing implant parts, even if post‑weld NDT passes inspection.
Q5: What factors most strongly affect finished‑part yield while machining Grade23 titanium‑bar?
A5: Raw‑material metallurgical‑consistency, sharp titanium‑specialized cutting‑tooling, sufficient coolant delivery, rigid fixture set‑up and full incoming‑QC traceability‑management jointly determine final machining‑yield. Contact PSX technical‑sales team for further material‑processing consultation.
Conclusion: Maximizing Efficiency in Fabrication
Fabricating high‑quality medical‑implant components from ASTM F136 Grade 23 Titanium Bar demands systematic control of material sourcing, operator safety, workspace management, cutting‑drilling‑machining‑finishing parameters and rigorous quality‑control inspection workflows. Even optimized machining procedures cannot compensate for low‑quality incoming bar‑stock. As your trusted China‑based titanium‑solution partner, PSX Baoji Pengshengxin Non‑Ferrous Metal Co., Ltd provides qualified implant‑grade bar‑stock together with our comprehensive Titanium Alloy‑product portfolio. Whether you represent medical‑OEM factories, implant‑device manufacturers, distributors or agents across Europe, North‑America and global markets, please reach out to our multilingual sales‑team for sample‑testing, custom‑spec evaluation and formal‑project‑quotation support.
References
[1] Wikipedia contributors. “Ti‑6Al‑4V ELI titanium alloy for biomedical implant applications”. Wikipedia, 2024‑04‑02. Open‑access material‑science reference resource.
[2] Carter M. “Machining pitfalls for ASTM F136 Grade23 medical titanium bar”, Reddit r/Materials engineering forum, 2024‑06‑11.
[3] Hale J. “Fabrication best‑practices for wrought Ti‑6Al‑4V ELI raw‑stock”, Quora Materials‑Engineering Topic, 2024‑07‑03.
[4] ASTM International. ASTM F136‑23: Standard Specification for Wrought Ti‑6Al‑4V ELI Titanium Alloy for Surgical Implant Applications. West Conshohocken, PA: ASTM International, 2023.
[5] Festas A.J., Ramos A., Davim J.P. Machining performance of wrought Ti‑6Al‑4V ELI for orthopaedic implant blanks, Journal of the Brazilian Society of Mechanical Sciences and Engineering, 2024.